A syrup capper that stopped the sticky mess
A Québec maple syrup producer losing more than 5% of bottles to a failing spindle capper. A new capper with vision inspection and a progressive reject system took rejects below 1%.

- rejects, down from over 5%
- <1% rejects, down from over 5%
- daily throughput
- +20% daily throughput
- changeover, tool-free
- 15 min changeover, tool-free
The problem #
Nokomis Maple Products of Trois-Pistoles works with more than 100 maple syrup producing families in the Bas-Saint-Laurent, one of the most northerly places in the world to produce maple syrup.
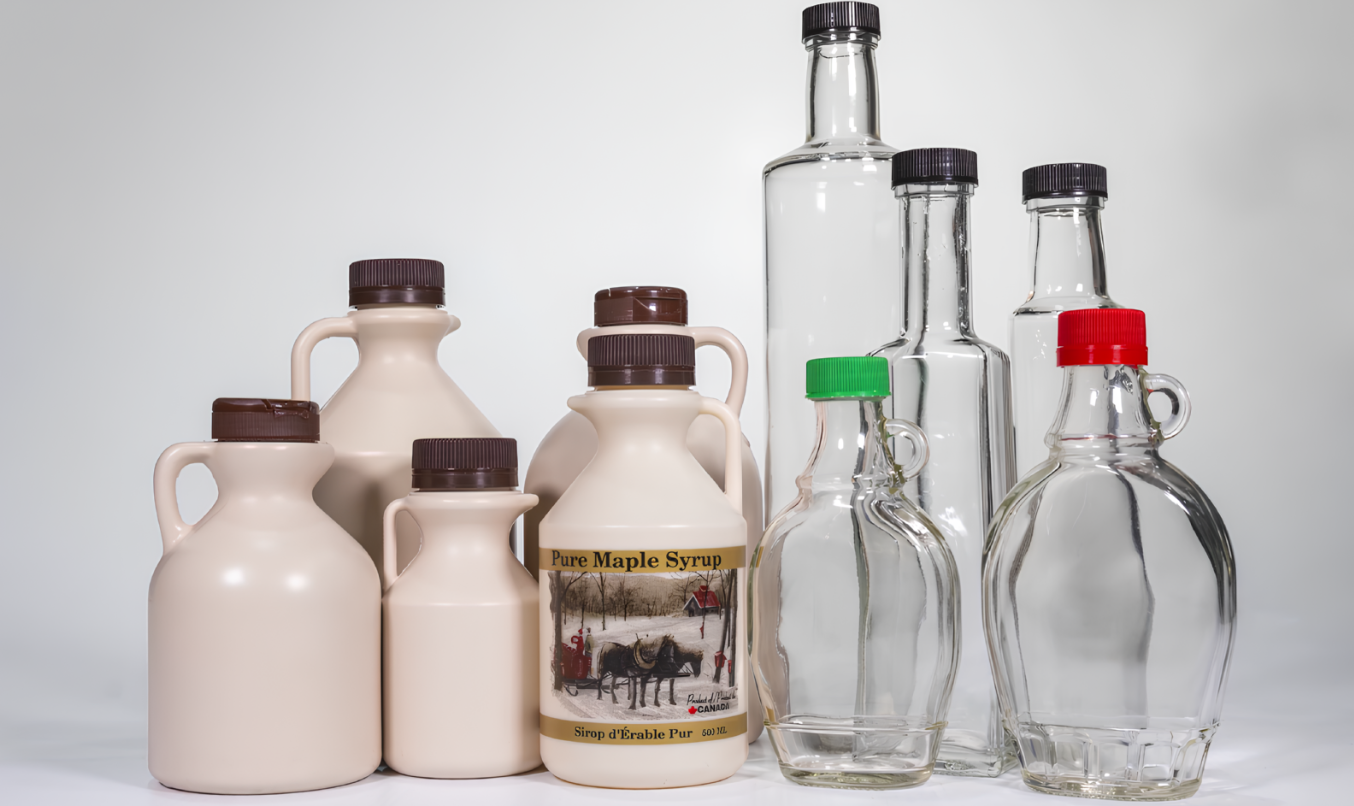
They fill a range of container sizes, from 189 mL glass bottles with an integral handle up to 1 L PP jugs. A six-head volumetric filler produces a natural bottle-to-bottle variation in fill height, which should not matter. But an inefficient spindle capper immediately downstream was rejecting more than 5% of bottles, and its six mechanical closers and two pneumatic clamping wheels left operators little room to measure or adjust.
What was installed #
Nokomis met three machine builders before choosing a Secure Chuck Capper from BellatRx. Vince More, VP at Nokomis, cited a solid track record with this type of machine, a very compact footprint, easy changeover and excellent reliability.
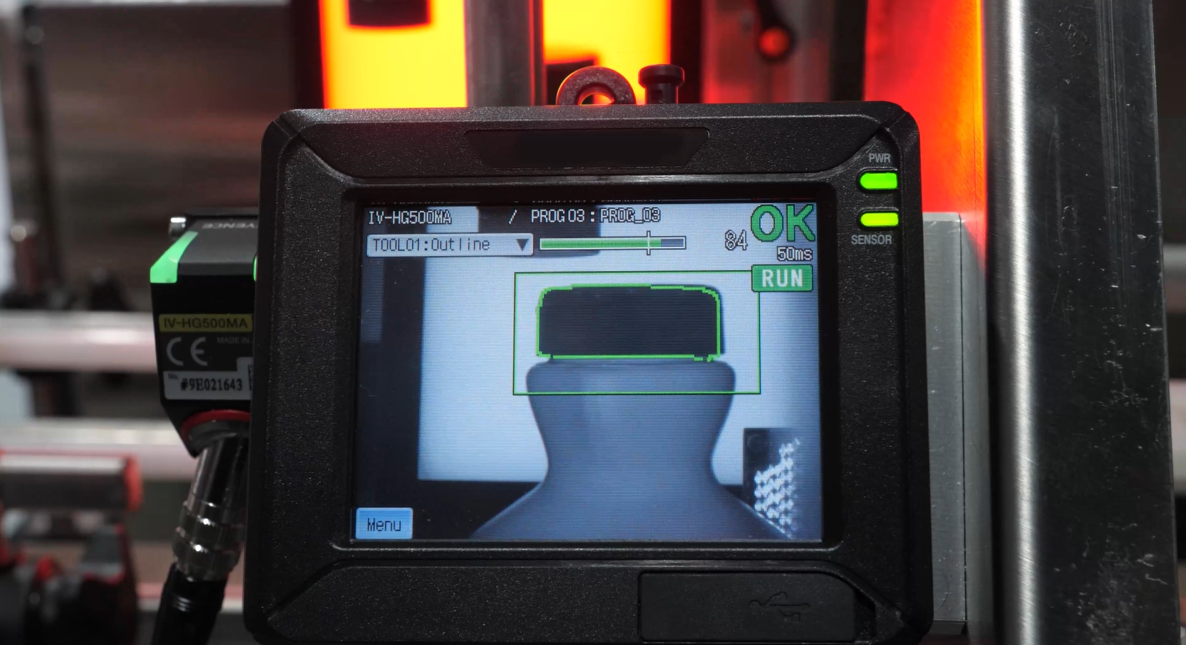
A camera inspection system checks both cap placement and fill level, with 100% of caps inspected before bottles leave the capper conveyor. An automatic progressive reject system removes non-conforming bottles without tipping them - critical when a spill means viscous syrup across the whole line.
Recipes and setup charts were built for each format, with discrete tooling locations so nothing needs tweaking during setup. Operators are ready to run in under fifteen minutes. Conveyors were designed to withstand periodic washdown.
The result #
Rejects fell from over 5% to under 1%. Daily throughput rose 20%, with the potential for another 20% over the following year. Staff who had been monitoring a high-reject capper and cleaning up spills were moved to other areas of the production floor.
Previously, all rejection detection was done at the end of the line during the final quality control. From now on, this automatic rejection system allows us to remove from the line a large part of the bottles with defects and improves the quality of the finished product.
Vince More, VP, Nokomis Maple Products